



Hangzhou Hezi Technology Co., Ltd.



News Center
Hezi technology focuses on the research and development of "rapid seamless conveyor belt joint sleeve" innovative technology project

NEWS CENTER
News Details
The Essential Guide to Belt Fasteners in the Rubber and Chemical Industry
Release time:
2025-10-30
In the rubber and chemical industries, the significance of effective fastening solutions cannot be overstated. One of the pivotal components in this domain is the belt fastener. Belt fasteners are essential for the assembly and maintenance of conveyor belts, which are widely used in manufacturing and processing plants. Understanding the different types of belt fasteners and their applications can
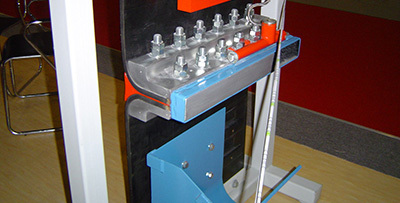
Belt fasteners come in various designs and materials, tailored to meet specific needs. Common types include mechanical fasteners, which are typically made of metal and can be installed without special tools, making them a convenient choice for many applications. These fasteners are designed to provide strong, reliable connections that can withstand the rigorous demands of industrial environments.
In contrast, vulcanized fasteners offer a more permanent solution, as they are chemically bonded to the belt material. This type of fastening is particularly beneficial for rubber belts used in heavy-duty applications, where resistance to wear and tear is critical. Vulcanized fasteners ensure a seamless connection that enhances the overall durability of the belt, making them ideal for use in environments that involve abrasive materials or extreme temperatures.
The choice of belt fastener can also significantly impact the speed of installation and maintenance. In industries where time is of the essence, opting for fasteners that allow for quick and easy installation can minimize production delays. Additionally, effective maintenance practices can prolong the lifespan of both the belt and its fasteners, leading to cost savings in the long run.
Moreover, the integration of belt fasteners in conveyor systems plays a vital role in ensuring the safe and efficient transportation of materials. In the chemical and rubber sectors, where product integrity is paramount, secure fastening can prevent issues such as material leakage or misalignment, which can lead to significant operational disruptions.
In conclusion, belt fasteners are a fundamental aspect of the rubber industry, influencing the performance and reliability of conveyor belts. By understanding the different types of fasteners available and their respective benefits, professionals in the chemical and rubber sectors can make informed decisions that enhance productivity and safety in their operations. As the industry continues to evolve, staying updated on advancements in fastening solutions will be crucial for maintaining a competitive edge.
Recommend News
Address
Address: No.82 Liangnong Road, Liangzhu street, Yuhang District, Hangzhou City, Zhejiang Province
Contact Information
Telephone:+86-571-88778905
Business consulting:+86-16657119700
Fax: +86-0571-88781967
Website
Website:www.hezikj.com
Official Mall:https://hzhlxjzp.1688.com/
Zip Code: 311113
Alibaba
Copyright © 2025 Hangzhou Hezi Technology Co., Ltd. | Powered by www.300.cn